English


What Are You Looking For?
A manufacturer of intelligent equipment needed slotted steel plates — laser-cut, with oval mounting slots and round holes — free of mill scale, slag and burrs on both faces, finished to a uniform hairline grain, without bending the plates or re-working the slots by hand. We engineered a custom 8-head flat grinding machine around the workpiece. This case study shows the configuration, the process flow and the result.
A flat plate grinding machine (also called a wide-belt or plate surface grinding machine) passes sheet-metal parts through a sequence of abrasive heads to remove scale, slag and burrs and produce a uniform brushed finish. For slotted steel plates that must be finished on both faces, we built a custom machine with 8 grinding heads in four stages — parallel abrasive belts for heavy stock removal, then upper and lower flap wheels for refinement on both sides — fed by an automatic feeder at a design rate of 200–400 metres per hour. The result: both faces finished in one pass, consistent grain from part to part, and no manual rework around the slots.
Most polishing-machine case studies talk about tubes, handles and cookware. This one is about something less glamorous and far more common: the plain steel bracket plate — the kind of laser-cut part that goes into trailers, machinery frames and mounting hardware by the thousands. It is also the kind of part that quietly eats an enormous amount of manual labour, because every face, every slot and every edge has to be cleaned up before the part can be sold.
Our customer is a Guangdong-based intelligent-equipment manufacturer that produces metal structural parts in volume. The workpiece in this project is a laser-cut steel plate with two oval mounting slots and round fixing holes, finished on both faces.
As it comes off the cutting table, the plate carries everything you would expect from thermal cutting:
The customer needed all of that removed, a uniform hairline grain on both faces, and edges and slots deburred — at a rate that keeps up with the cutting machine downstream, without thinning or distorting the plate.
Grinding the flat face of a plate is easy. The hard parts are the edges of the oval slots and holes (burr removal without enlarging or rounding over the cut), and flatness — aggressive grinding on a thin plate generates heat and pressure that can bow the part. The machine configuration has to solve both.
Before automation, this kind of part is typically finished on hand-held angle grinders or bench grinders. That works for hundreds of pieces. It stops working at thousands, for four predictable reasons:
The customer's requirement list was therefore straightforward in intent and demanding in detail: automatic feed, both faces finished in one pass, burr-free slots, a repeatable hairline grain, and throughput of 200–400 metres of plate per hour. That combination is exactly what a multi-head flat grinding machine is designed to deliver.
We engineered the machine around the workpiece rather than selling a standard model, because the plate's thickness, slot geometry and required finish dictated the head sequence. The machine processes the parts in a straight line — feed → grind → refine → output — with eight grinding heads in four functional stages:
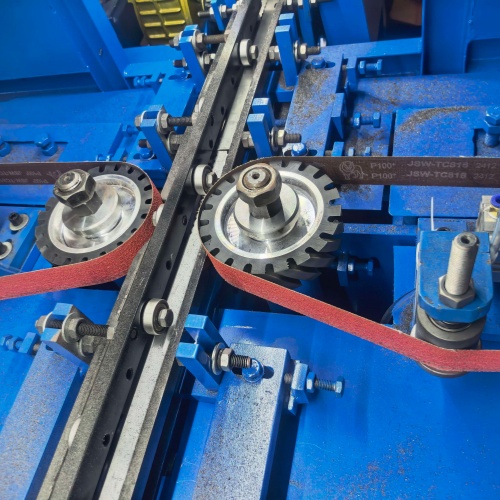
One set of two abrasive belts running in parallel (left and right) takes off the heavy work: mill scale, slag and cutting burrs. The belts are tension-adjustable, and the heads can oscillate vertically so the belt tracks across the full plate width and never cuts one groove.
One set of two thousand-page (flap) wheels in parallel erases the belt marks and starts the hairline grain. These heads run with automatic pressure compensation, so contact force stays constant as the wheels wear.
Two upper flap wheels refine the top face. They oscillate left–right to blend the grain evenly across the surface, with automatic pressure and optional vertical oscillation to fine-tune the contact.
Two lower flap wheels mirror the same treatment on the underside — which is how both faces of the plate come out finished in a single pass, with no flipping of the workpiece.
A motorized feeder presents the plates to the first head at a controlled, constant speed, and the finished parts leave the outfeed end ready for packing. The full specification:
| Item | Configuration |
|---|---|
| Machine type | Custom flat plate grinding / deburring machine (multi-head, inline) |
| Workpiece | Laser-cut steel plates with oval slots and round holes; both faces to be finished |
| Total grinding heads | 8 |
| Stage 1 | 1 set of parallel abrasive belts (2 belts, left + right) — tension adjustable, vertical oscillation |
| Stage 2 | 1 set of parallel flap wheels (2 wheels) — automatic pressure, optional vertical oscillation |
| Stage 3 | 2 upper flap wheels — left–right oscillation, automatic pressure |
| Stage 4 | 2 lower flap wheels — left–right oscillation, automatic pressure |
| Feed system | Motorized feeder with conveyor |
| Design efficiency | 200–400 m/hour feed rate |
| Process flow | Feeder → parallel belts → parallel flap wheels → 2 upper flap wheels → 2 lower flap wheels → output |
| Commissioning | Installed and commissioned at our factory; customer operators trained on site |
| Warranty | 180 days on the complete machine; 90 days on bearings |
Configuration shown is the one built for this project — head count, abrasives and oscillation are selected per workpiece.
The division of labour between head types is the core of the design. Abrasive belts cut — they remove scale and heavy burrs fast and flat. Flap wheels refine — their compliant construction follows the surface and produces the fine, even grain that belts cannot, including into the edges of slots where a stiff belt would only ride over. And because the machine carries heads on both the upper and lower sides, the second face is finished by the machine, not by a second operator.
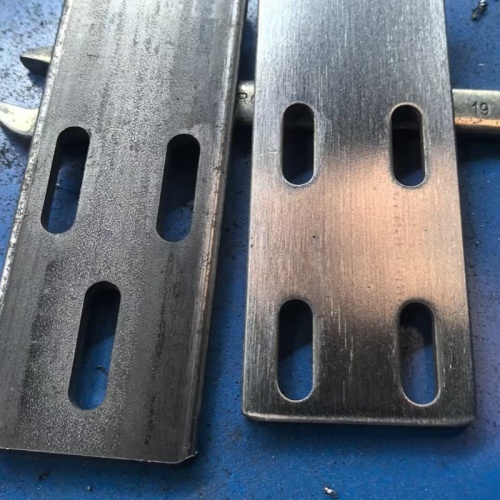
The difference is easiest to see on the parts themselves. On the untreated plate, the surface is dark and patchy with mill scale, the slot edges carry slag, and the overall look is rough and inconsistent. After one pass through the machine, both faces show the same even, directional hairline grain, the slot and hole edges are clean and deburred, and the plate stays flat.
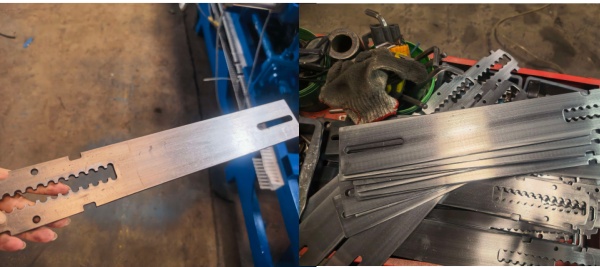
Just as important for the customer is what the machine does between the parts: nothing. No operator judgement, no variation in pressure or angle, no queue at the finishing bench. Every plate that leaves the outfeed end has the same grain, the same edges and the same flatness as the one before it — which is precisely what their downstream assembly (and their customers) are paying for.
Custom does not mean open-ended. Our custom-machine process runs in five fixed steps, and this project followed it exactly:
You send the part — a drawing, a photo or better still a physical sample — plus the finish you need and your target throughput. We assess material, thickness, slot geometry and current finishing method.
We propose the head sequence, abrasives and machine layout, with a dimensioned scheme drawing you can review against your shop floor. This is the step where the 8-head configuration above was agreed.
We install and commission the machine in our own works, running it until the process is stable before you ever see it.
You send people to our factory, inspect the machine running your parts, complete the initial acceptance, and your operators are trained to run it competently before it ships.
The machine ships film-wrapped, with 180 days of whole-machine warranty and 90 days on bearings, and our team stays available for consumables and process adjustments.
Notice what this structure buys you: you sign off on the machine running your own workpiece before it leaves our floor. The risk of "it works in the demo, but not on my parts" is designed out, not hoped away.
Whether your parts look exactly like these plates or not, the same four questions decide the machine configuration:
Send us the answers — ideally with a sample part — and we will come back with a configuration and a scheme drawing, exactly as we did here.
Send us the workpiece — a sample, a drawing or a photo — and the finish you need. We will propose a machine configuration with a scheme drawing, run it on your parts before delivery, and train your operators until they can run it blind.
Request a Custom Grinding Machine ProposalLeave A Message
Scan to Wechat :
Scan to WhatsApp :